
Silo Walkway Anti-Slip Safety Improvement
A practical, fast-deploying anti-slip treatment for a silo access walkway that had become hazardous in wet and dusty conditions — now being rolled out to further walkways across the site.
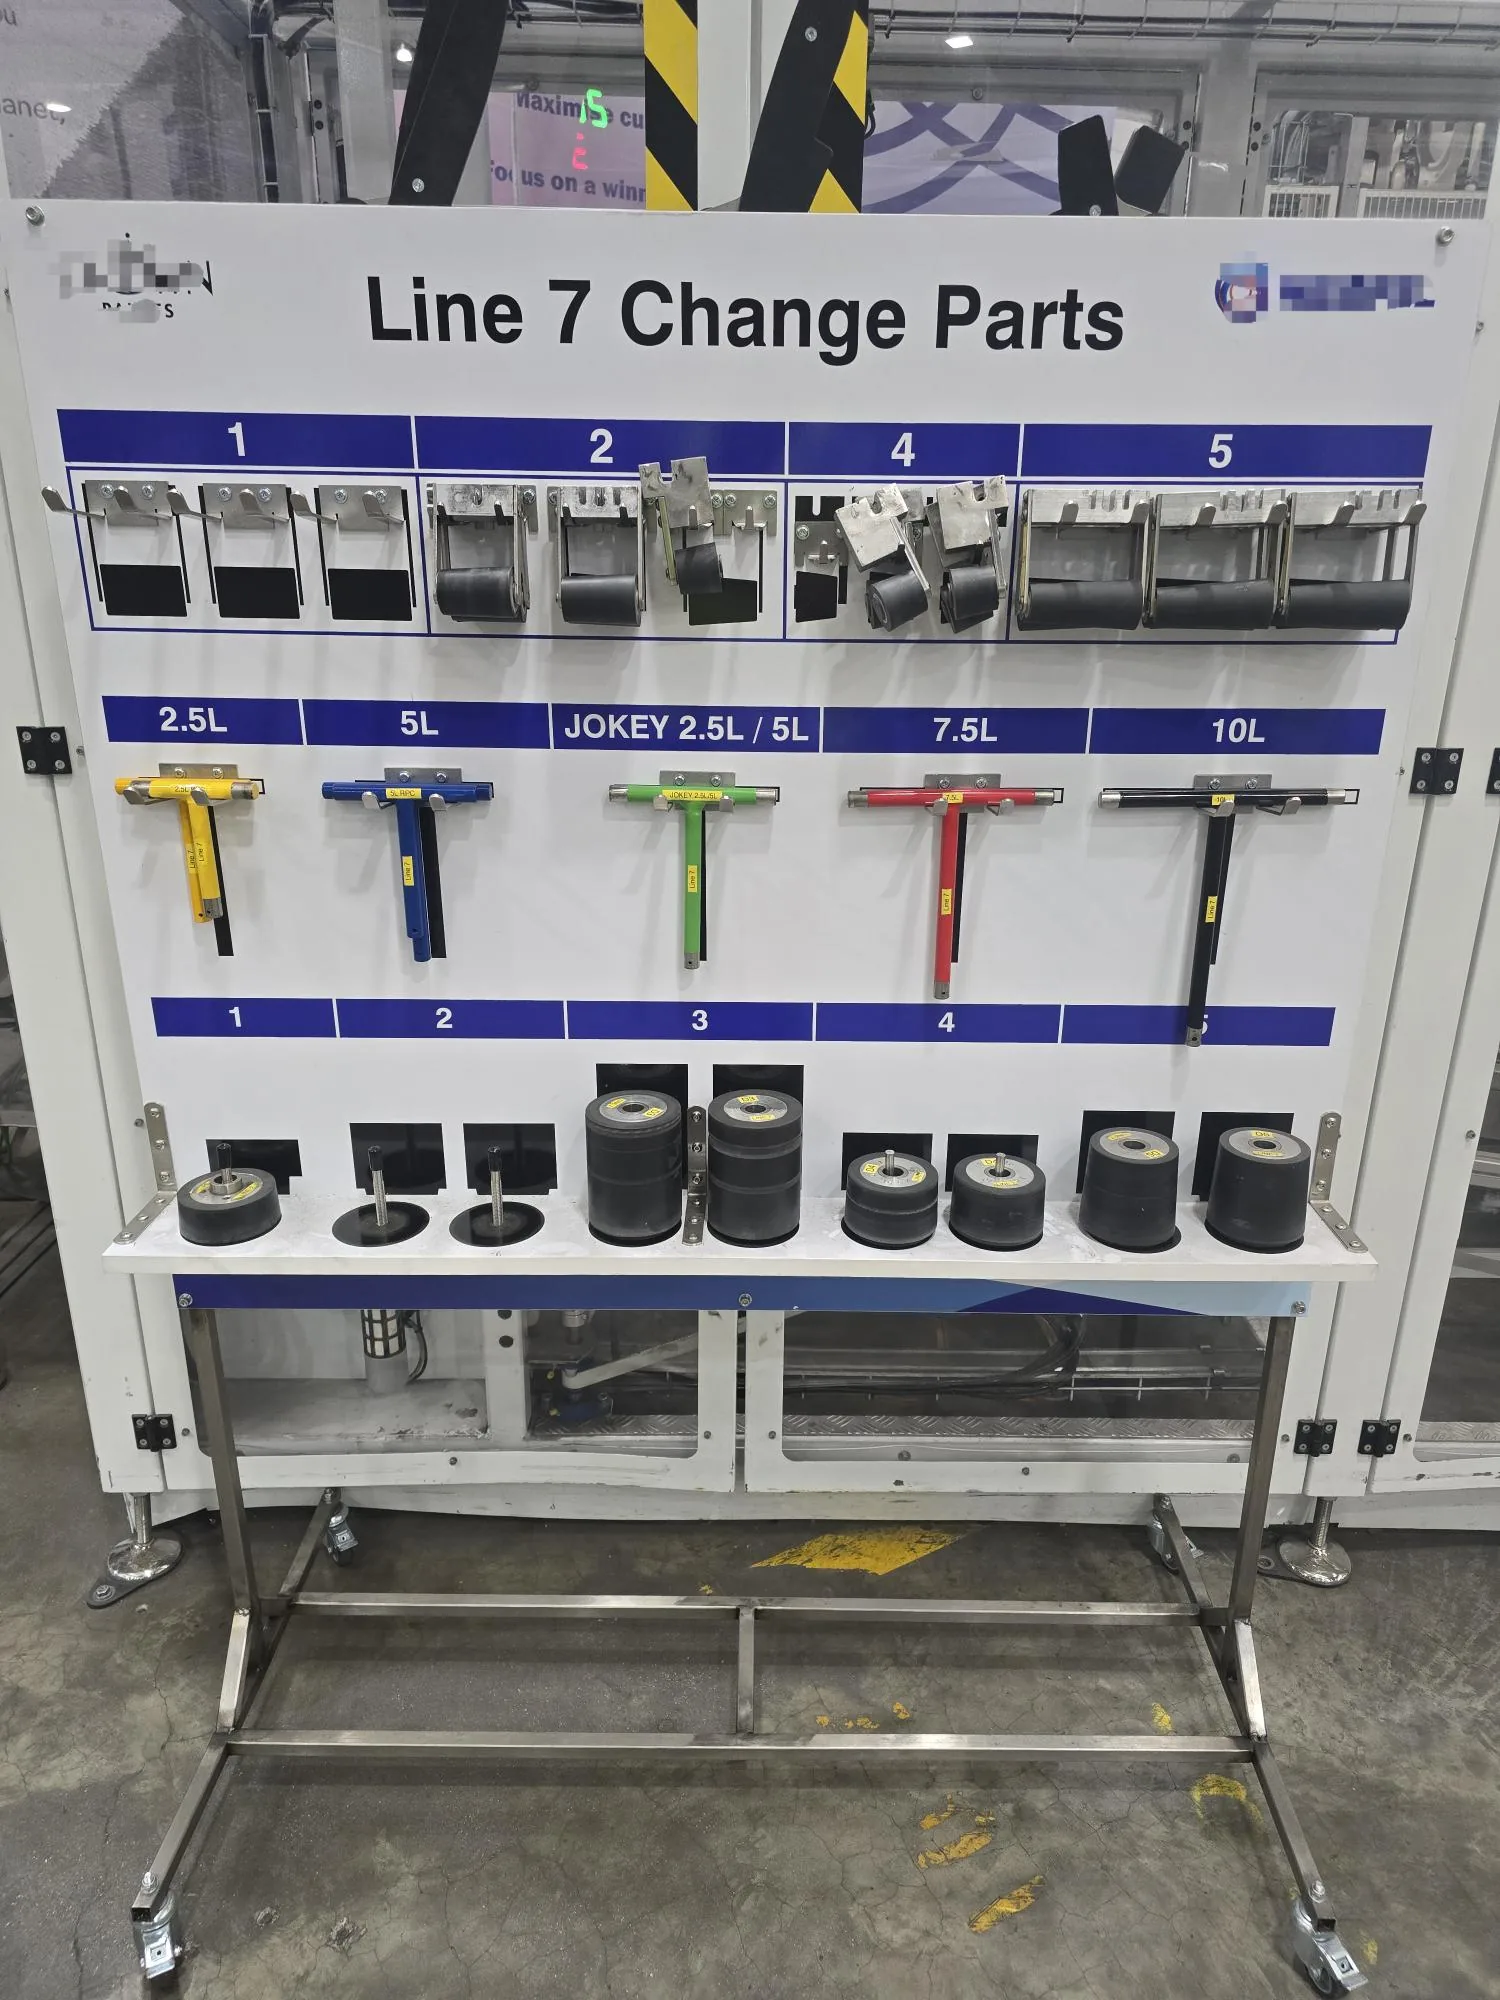
View Case StudyA practical 6S and changeover improvement project within a high-volume manufacturing facility — bespoke mobile shadow boards brought tools and change parts to the point of use, reducing search time and supporting faster, more repeatable changeovers.
As part of a wider Continuous Improvement and 6S programme within a high-volume manufacturing facility, DEVA Maintenance was asked to support improvements to production line changeovers. A review of the existing process identified opportunities to reduce wasted movement, searching time and unnecessary delays caused by tools and change parts not being consistently organised or positioned at the point of use. These small losses were contributing to longer changeover times and reducing overall production availability.
Working around the requirements of the production teams, DEVA Maintenance identified the tools and change parts required for each line and developed practical improvements to support faster, more consistent changeovers. The project included:
The completed system provided production and engineering teams with a clear, standardised location for the tools and change parts required during line changeovers. By reducing time spent searching for equipment, improving point-of-use availability and standardising the changeover setup, the project helped reduce non-value-added activity during planned production stops.
The mobile design also allowed the shadow boards to be moved between suitable working positions, giving the production teams flexibility without losing the benefits of standardised organisation.
A practical, fast-deploying anti-slip treatment for a silo access walkway that had become hazardous in wet and dusty conditions — now being rolled out to further walkways across the site.
View Case StudyControl cams that had fallen out of sequence were causing product overflow and switch contamination. The assembly was stripped, cleaned, re-timed and tested, with permanent reference marks added for quicker future calibration.
View Case Study